Batch consistency in manufacturing often begins with a deceptively simple repeat-order instruction: “same SKU as last time.” When I reopen a finished projector program, I need to know which version, power path, included set, labels, controlled files, packing configuration and buyer acceptance record made the first batch acceptable. Otherwise, the new purchase order names a product but not its approved state.
The risk becomes more visible when downstream customers can place units from two deliveries beside each other, or when the buyer has promised the same SKU under the same listing or project specification. A difference may be harmless, approved or necessary. The control problem is whether the difference entered the repeat order visibly and whether somebody had authority to accept it.
Batch consistency in manufacturing is a traceable comparison between one approved batch state and the next—not a universal consistency percentage. Freeze the exact SKU, version and configuration; retain a usable approved reference; define the buyer's measurable acceptance method; log material, process and document changes; compare the repeat batch under the same method; and give every deviation a disposition before release.
That chain does not prove that every unit is visually or numerically identical. It also does not assume that a component change, line changeover or document revision has occurred at Bowlum. Those are general change-control mechanisms a buyer should be able to see if they become relevant. This article begins after supplier onboarding and first-batch closeout. Its single question is narrower: how can the buyer verify that a second or later batch of the same approved product contains no unapproved change?
What Does Batch Consistency in Manufacturing Mean for a Repeat Projector Order?
The word consistency can hide two different decisions: whether today's units meet today's release requirements, and whether those requirements still represent what the buyer approved before.
For a repeat projector order, batch consistency means that the next batch can be traced to the same approved identity and evaluated against the same acceptance basis, with every proposed or observed difference recorded and dispositioned. It is not a claim that two batches are perfectly identical, and it is not a default percentage that can be copied from another product.
I separate two questions that are often compressed into the word “quality.” The first is whether units in the current batch meet the released requirements. The second is whether the released requirements, components, methods and documents still represent the state the buyer approved before. A batch can pass its current factory checks while the buyer still lacks evidence that an unannounced revision did not enter the program.
That is why I build the repeat-order decision around five continuities:
| Continuity | Question for the repeat order | Evidence needed before release |
|---|---|---|
| Identity | Is this the same public SKU, selected version and sellable configuration? | Dated configuration record tied to the purchase order |
| Reference | What exactly represents the first approved state? | Indexed physical and/or digital reference package |
| Method | Will both states be checked in the same defined way? | Buyer-approved method, conditions, tools and record format |
| Change visibility | Were any material, process or document deltas proposed? | Dated delta register with owners and approval states |
| Disposition | Who decides what happens when a difference appears? | Accept, correct/recheck, controlled-change approval, or hold/escalate decision |
The word “same” becomes auditable only when all five are connected. A photograph can help identify a visible housing. A purchase order can identify a commercial line. Neither one alone tells me which control version, adapter, packing arrangement, instruction file or acceptance method was approved.
This distinction also prevents an unfair conclusion. A visible difference is not automatically a defect, and a document revision is not automatically evidence of poor control. The buyer first asks whether the delta was within the frozen scope, whether it was disclosed, and whether the agreed method accepts it. Only then is there a basis for a release decision.
I do not release a repeat order on “everything looks the same.” I release it when the approved state, comparison method, change record and decision still point to the same product promise.
Why Is the Exact SKU Still Not a Complete Repeat-Order Baseline?
A reorder can preserve the public product code while leaving the version or supplied configuration unstated.
A public SKU is the anchor for repeat-order identity, but it may not identify the selected version, controls, power path, included accessories, labels, files or packing configuration. The repeat baseline must freeze those executable choices beside the SKU so that procurement, production and inspection are comparing the same sellable unit.
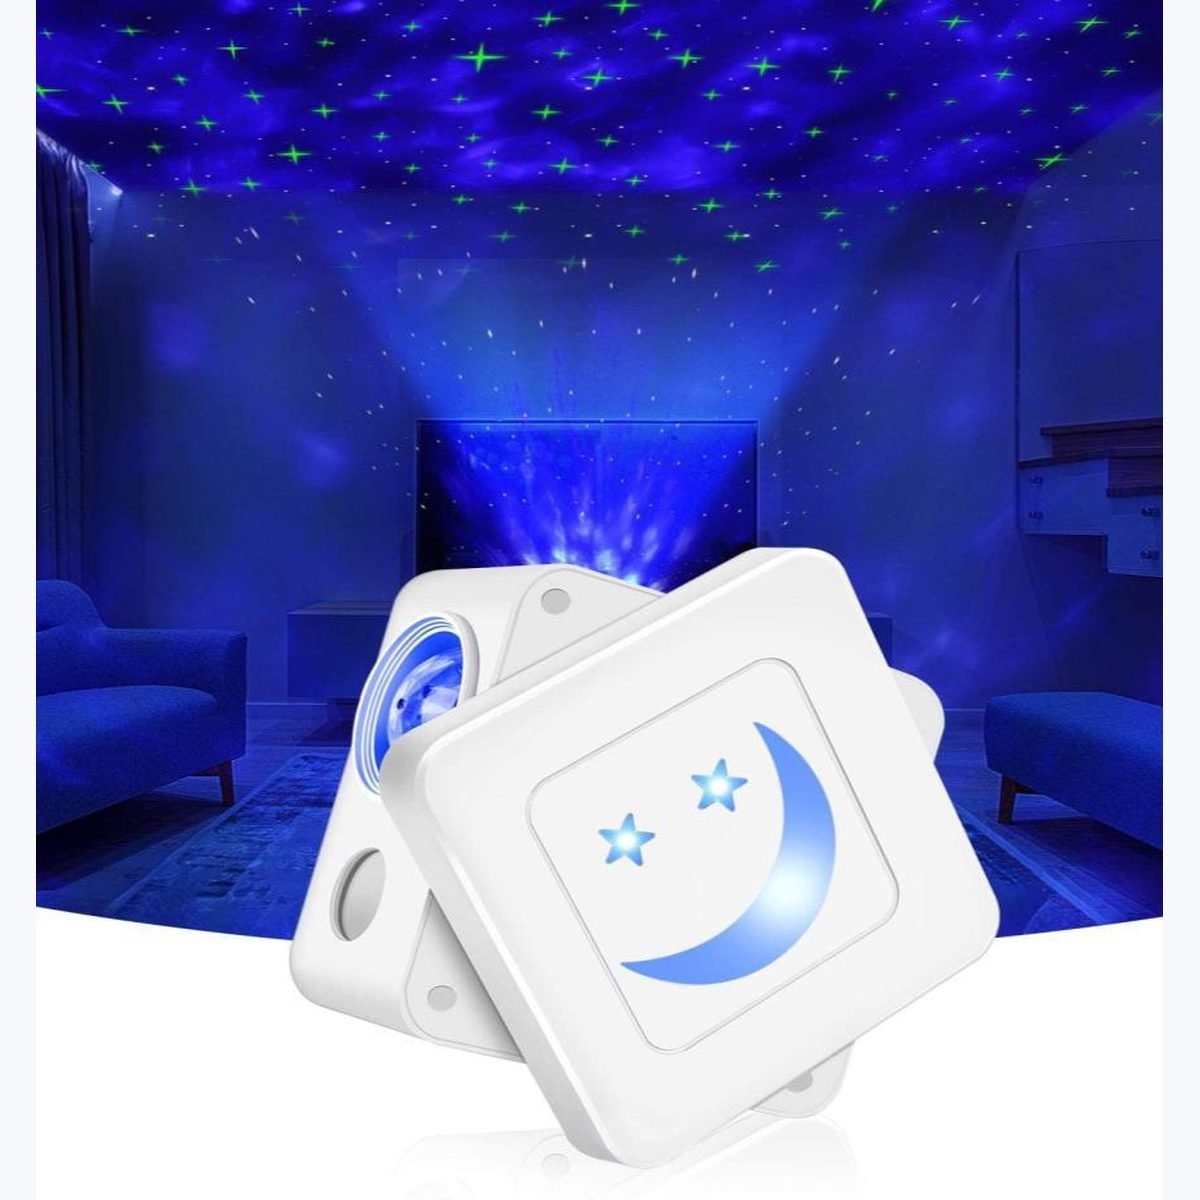
BWL-OL-004 makes the version problem concrete. Its public product title includes a 7-color APP family version and a DMX512 professional version. Writing only BWL-OL-004 on a reorder does not choose between those two sellable contexts. BWL-SP-011 shows a different identity boundary: its current data contains valid 12-piece and 16-piece master-carton configurations. Its public SKU does not tell a logistics or inspection team which packing plan the buyer selected.
I do not use either example to claim a batch difference occurred. I use them to show that identity has layers. Before a repeat order is released, I recover the approved value at each layer that can change what the buyer receives or how the product is accepted.
| Baseline layer | What I freeze | Why the SKU alone may be insufficient |
|---|---|---|
| Product identity | Public SKU and named sellable version | One SKU may contain more than one control or market-facing version |
| Power path | Approved input requirement, adapter identity, plug and included cable set | A compatible-looking accessory is not automatically the approved supplied set |
| Controls and content | Control mode, approved functions and controlled file revision where relevant | The housing can stay familiar while the user-facing behavior or file changes |
| Included set | Mounts, remotes, accessories and buyer-approved exclusions | A product line can be correct while its sellable set is not |
| Presentation | Housing/color reference, labels, artwork and instruction revision | Listing continuity depends on more than internal function |
| Packing | Inner arrangement, master-carton configuration and shipping marks | One SKU may have more than one valid packing route |
| Acceptance | Named check, conditions, evidence format and approver | A result cannot be compared when the method has changed silently |
The power row remains a system boundary, not a side note. The buyer should preserve the exact approved adapter and cable identity without turning a nearby label, a housing photo or another SKU's file into evidence. The deeper adapter verification method belongs to its own engineering review; here I record only which approved power configuration the repeat batch must reproduce.
I also record the baseline revision and approval date. “Latest” is not a useful state when the buyer and factory hold different files. A repeat-order packet should point to one controlled version and name any later approval that supersedes it. If a field is intentionally open, I mark it open rather than letting a team member fill it from memory.
What Should the Buyer Retain From the First Approved Batch?
A sample becomes useful only when the next reviewer can tell what it represents and how to compare against it.
Retain a reference package, not just a sample on a shelf. The package should identify the approved physical reference when one is appropriate, the exact controlled files, the test or comparison method, the conditions used, the first-batch record, the approvers and the location of every item needed to reproduce the decision.
The projector supplier onboarding checklist owns the first configuration freeze and first-batch handoff. For repeat-order work, I take the closed first-batch packet as the starting point and ask a different question: can another reviewer reconstruct why that state was approved without relying on the memory of the person who was present?
A physical unit can be valuable, but it is not self-explanatory. It can age, be handled, lose accessories or become separated from the file revision and test conditions that gave it meaning. A photograph is easier to store but may hide dimensions, surface differences, control behavior or included components. A report can preserve readings while omitting which unit, setup or revision was checked. The retained reference therefore needs an index.
| Reference component | What the index records | What it does not prove by itself |
|---|---|---|
| Physical reference, when used | Identifier, holder, condition, sealed/open state and dated images | That its appearance is a measurable acceptance method |
| Approved configuration sheet | SKU, version, power, controls, included set, presentation and packing | That production followed it |
| Controlled files | Filename, revision, approval date and responsible owner | That the correct file was applied to the repeat batch |
| Comparison method | Attribute, setup, condition, tool/checklist, record format and decision owner | A universal tolerance for another program |
| First-batch evidence | Unit/batch identity, result, exceptions, disposition and evidence location | Future conformity without a repeat comparison |
| Approval record | Who accepted what, when, with which open conditions | Permanent approval of later undisclosed changes |
I ask the buyer to decide which attributes actually need physical retention and which are better controlled through files and repeatable measurements. Appearance may need a protected physical reference plus controlled lighting. Function may need a named sequence and a result record. Packing may need an approved pack-out sheet and images. Labels and instructions usually need source files or approved proofs, not a photograph of a closed carton.
Bowlum has one narrow confirmed retained-sample fact that should not be stretched. In our housing-color-only customization path, the buyer signs the approved color sample and the buyer and factory each retain one before bulk production is compared with it. Our color-versus-new-tooling guide explains that specific project boundary. I do not claim from it that every standard order automatically receives a two-sided retained sample.
The repeat-order method in this article is therefore a buyer requirement. It can be adopted for a project whether the useful reference is a physical unit, an approved file set, a measurement record or a combination. The test is not whether somebody says a “golden sample” exists. The test is whether the reference can be identified, preserved and used under a defined comparison method.
How Should Material, Process, and Document Changes Be Logged?
A repeat-order team can overreact to every difference or overlook a meaningful one when there is no common place to declare and approve deltas.
Use one delta register that asks what was frozen, what may change, why the change is proposed, which evidence is affected, who must approve it and whether the repeat order may proceed. Treat substitution, changeover and document revision as generic risk mechanisms—not as proof that any such event occurred at Bowlum.
When I ask “what changed?”, silence is not the same as a controlled answer. I give the supplier and buyer a structured way to state that a field is unchanged, that a change is proposed and pending, or that a change has already been approved. This avoids two opposite errors: assuming every repeat batch contains hidden substitutions, and assuming a familiar SKU guarantees that nothing could differ.
The register covers three change families because each can alter a different part of the buyer promise:
- Material or component delta: a component identity, supplier reference, finish, accessory or packing material may be proposed for change. The register names the affected requirement and comparison evidence without asserting that a change has occurred.
- Process delta: an assembly instruction, setting, fixture, inspection step or production route may be revised. The important point is the approved method and output requirement, not an unsupported promise that every order will remain on one line.
- Document or file delta: a label, manual, artwork, controlled software/content file, inspection sheet or packing document may receive a new revision even when the exterior remains familiar.
| Delta-register field | Required entry | Release meaning |
|---|---|---|
| Frozen item | Baseline identifier and revision | Defines the approved starting state |
| Proposed/observed delta | Specific difference, or an explicit no-change statement for the reviewed scope | Prevents “same” from remaining an assumption |
| Reason and affected boundary | Why it is proposed and which requirement/evidence may change | Routes the right technical and commercial review |
| Evidence required | Updated file, sample, measurement, inspection or other named proof | Defines what must be reviewed, without inventing the result |
| Approval state | Unchanged / proposed-pending / approved / observed-not-preapproved | Makes authority visible |
| Decision owner and date | Named buyer/factory roles and dated decision | Prevents informal acceptance from becoming the record |
| Downstream updates | Purchase order, specification, artwork, inspection or packing record to revise | Keeps documents from describing different product states |
I do not make production-line identity a shortcut for this register. The same line would not prove that materials, work instructions, files or settings stayed fixed. A different line would not prove that the approved output changed. The evidence chain must follow the frozen configuration and acceptance method, regardless of where a buyer and factory agree to execute the work.
I do not accept a story about why a repeat batch should be the same. I ask for a delta record showing what stayed frozen, what changed with approval, and which evidence closes the buyer's requirement.
How Should Batch Consistency in Manufacturing Be Compared From the First Batch to the Next?
Two sets of results cannot support a batch-to-batch decision when they were created under different methods or conditions.
Compare the next batch with the approved first-batch reference under the same named method, conditions and evidence format. Define the project's attributes and decision rules before inspection; do not import a brightness, color, pattern, cosmetic or dimensional tolerance from another projector or publish a generic “consistency rate.”
Side-by-side comparison matters when the buyer's downstream channel can put two deliveries together or expects one SKU promise to persist. But “put them side by side” is still not a method. I require the comparison record to say which attribute is checked, how the condition is controlled, which reference is used, what evidence is saved and who decides the result.
| Comparison area | First approved reference | Repeat-batch record | Buyer-defined decision basis |
|---|---|---|---|
| Identity and construction | Frozen SKU/version/configuration and approved evidence | Unit/batch identity plus current configuration record | No unapproved identity or construction delta |
| Power and controls | Approved power path and functional sequence | Same named sequence and evidence format | Project requirement agreed for this configuration |
| Projection or visible output | Approved setup, condition and reference record | Result captured under the same approved method | Project-specific acceptance rule; no borrowed default |
| Housing and presentation | Approved physical/file reference and viewing condition | Dated evidence linked to inspected identity | Buyer-approved appearance method and exceptions |
| Labels, instructions and files | Approved revisions | Applied revisions and verification record | Exact approved or explicitly superseding revision |
| Included set and packing | Released component list and packing plan | Current pack-out/marking record | Same approved set or controlled approved delta |
For an optical attribute, I do not compare images captured at different distances, ambient conditions, camera settings or product states and call the result objective. The buyer should use the method already approved for that product. If the project never defined one, the correct action is to define and approve it before the repeat-batch result is used—not to borrow a number from another SKU.
Sampling also belongs to the buyer's project method. This article does not prescribe how many units to select or which tolerance to apply because product risk, contract scope, inspection stage and downstream use can differ. The record should identify the selection method actually agreed, the units checked and the limits of the conclusion.
I keep source facts and decisions in separate columns. A captured observation tells the reviewer what was seen or measured. The approved rule tells the reviewer how to interpret it. The disposition tells production or procurement what happens next. Combining all three into a single pass cell makes later comparison difficult, especially when an exception was accepted for one batch but never added to the baseline.
The most useful output is a first/next-batch comparison sheet with four visible states: matched under the approved method, approved change, unresolved deviation, or not evaluated. “Not evaluated” is not failure; it is an evidence boundary. It stops an empty field from being treated as proof of consistency.
What Do Bowlum's Unit-Level Release Checks Prove—and Not Prove?
Factory release checks and buyer batch-comparison checks can both be real while answering different questions.
Bowlum's roughly eight-hour aging for every unit and its per-unit Class 1 release process for laser products are factory release controls. They do not prove that two batches are identical, that no specification changed, that a product will last for a stated period, or that one model's test or certification applies to another.
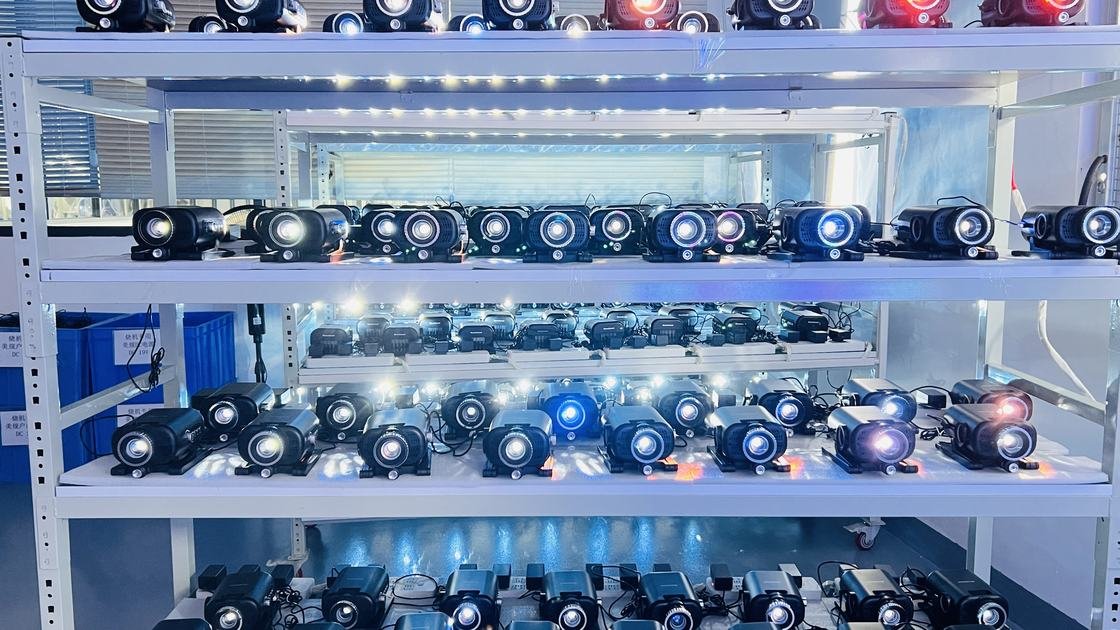
I include these facts because release control and repeat-order consistency are often confused. Bowlum confirms that every unit receives roughly eight hours of aging before shipment. That supports a per-unit factory release step within its stated process. It does not demonstrate service life, field reliability, a lower defect rate, or equivalence between the first and repeat batch.
For products that use laser sources, Bowlum also confirms an in-house laser test room and a process in which every laser product must meet Class 1 before shipment. I treat that as a unit-level release boundary for the applicable laser product. I do not use it as a blanket certificate statement for BWL-OL-004, BWL-SP-011 or any other named model, and I do not transfer it to a non-laser product.
| Control | What the confirmed process supports | What it does not support |
|---|---|---|
| Roughly eight-hour aging on every unit | A per-unit aging release step occurred within the factory process | Lifetime, field performance, avoided failures, a defect rate or cross-batch equivalence |
| Per-unit Class 1 release for laser products | Applicable laser units must meet the factory's Class 1 shipment-release process | Certification for another SKU, optical sameness, performance equivalence or non-laser coverage |
| Buyer first/next-batch comparison | The recorded attributes were compared under the buyer's approved method | Attributes not evaluated, future batches or a universal consistency percentage |
| Delta register | Proposed and observed changes in the reviewed scope are visible for disposition | Proof that no unreviewed condition exists outside that scope |
The controls answer different questions and should remain separate. Unit-level release asks whether each applicable unit cleared the factory step. Batch-to-batch comparison asks whether the approved product state and buyer-facing result remained inside the agreed boundary. Change control asks whether a delta was disclosed and authorized. Passing one column does not automatically close the others.
This separation protects the strength of the real factory facts. Aging remains a concrete per-unit release control instead of being inflated into a lifetime claim. The laser process remains tied to applicable units instead of becoming cross-model certification language. And the buyer's consistency method remains accountable to its own reference, conditions and decision rule.
What Should Happen When a Repeat Batch Deviates?
A difference becomes manageable only after the team separates the observation from its cause and from the authority to release it.
A repeat-batch deviation needs a named disposition, not an automatic accusation or silent waiver. The buyer and factory should identify the affected requirement, preserve the evidence, decide whether to accept, correct and recheck, approve a controlled change, or hold and escalate, then update every baseline record that the decision legitimately supersedes.
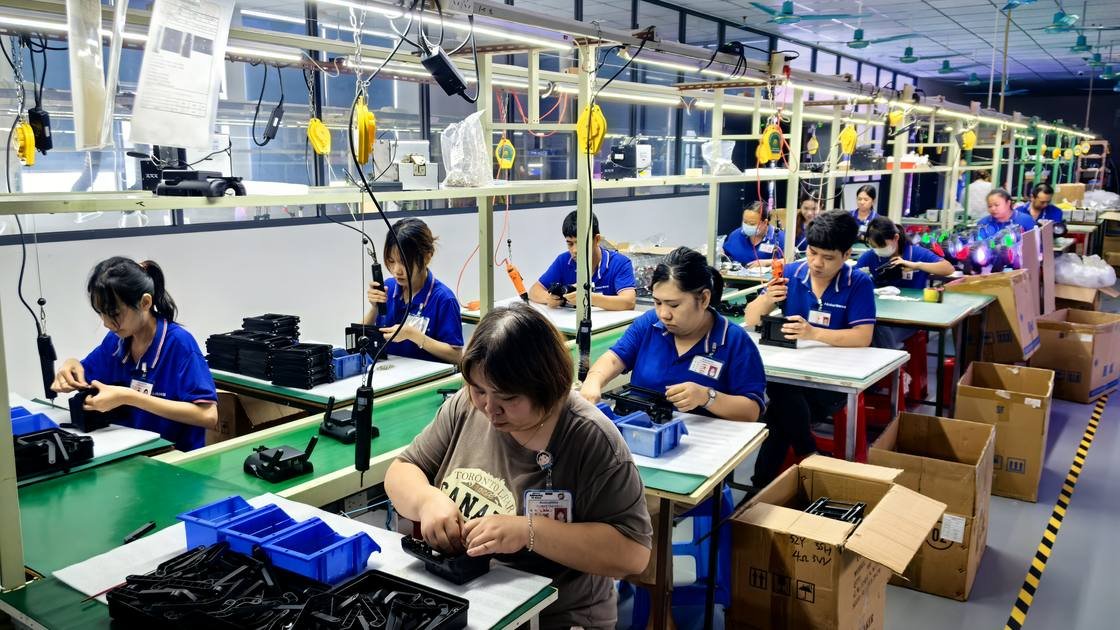
When a difference appears, I first preserve its identity: exact SKU/version, batch or unit reference, comparison method, condition, observation and evidence location. I do not label a component, process or supplier as the cause from appearance alone. If the difference becomes a suspected defect pattern, the published projector batch-defect and return-log guide owns the deeper reproduction and cause-separation method.
For repeat-order release, the disposition can stay operational:
| Disposition | When it applies | Required record before release |
|---|---|---|
| Accept as matched | Evidence meets the existing approved decision basis | Comparison result and approver |
| Correct and recheck | The current state can be brought back to the frozen requirement | Correction record, repeated check and new result |
| Approve as controlled change | The buyer accepts a proposed difference as the new state | Approval, affected documents and superseding baseline revision |
| Hold and escalate | Evidence is incomplete, impact is unresolved or authority is missing | Hold scope, owner, open question and next decision gate |
An approved exception should not disappear into an email. The record must say whether it applies only to the inspected batch or replaces the baseline for future repeats. Otherwise, the third order can accidentally treat a one-time waiver as the permanent product definition.
A Repeat-Order Case: An Outdoor Lifestyle Brand Replaced “Same as Last Time” With a Comparison Gate
A product lead at a US outdoor lifestyle brand showed me a repeat-order brief for an outdoor-projector program. The main instruction was “same as last time.” The team could locate a prior product record and presentation files, but that sentence did not identify which retained evidence represented approval, which method would compare the next batch, or how an allowed change would be distinguished from an unresolved difference.
I did not promise that a repeat run would be identical or prescribe a consistency percentage. I rebuilt the question in three connected records. First, the retained-reference index named the approved SKU/version/configuration, physical or file references, first-batch evidence and responsible holders. Second, the delta register required an explicit state for material, process and document fields. Third, the comparison gate named the attribute, condition, evidence format, decision owner and possible disposition.
The product lead's question changed from “Can the factory make it the same?” to “Which approved state is being repeated, which deltas are declared, and what evidence closes each comparison before release?” The working packet ended at that auditable gate rather than assuming a production or commercial result.
The method gave the team a disciplined place for uncertainty. An unchanged field could be confirmed. A proposed delta could wait for approval. An observed difference could be held without being called a defect before investigation. A buyer-approved change could supersede the correct files without rewriting the history of the first batch.
I close a repeat-order release only when the baseline, delta register, comparison evidence and disposition all describe the same approved product state.
Conclusion
Repeat-order batch consistency is not a personality test for a supplier and not a percentage to borrow from another product. I start with the closed first-batch record, expand the public SKU into the exact approved version and configuration, retain a usable reference package, and require one measurable buyer method for the first/next-batch comparison. Material, process and document differences enter a delta register; every deviation receives a visible disposition. Bowlum's per-unit aging and applicable laser release controls remain important factory checks, but they do not replace that comparison or prove cross-model equivalence. My release rule is simple: no repeat batch becomes “same as last time” until the approved baseline, declared changes, comparison evidence and decision record agree.
Frequently Asked Questions
What is batch consistency in manufacturing?
For a repeat order, it is a traceable comparison between the approved first-batch state and the next batch. The method connects exact identity, retained references, buyer-approved checks, declared changes, comparison evidence and deviation disposition. It is not a universal percentage.
Is using the same projector SKU enough for a repeat order?
No. The baseline should also identify the selected version, power path, included set, controls, labels, controlled files, presentation and packing configuration. One public SKU may contain more than one valid sellable or packing context.
Does every repeat order need a golden sample?
It needs a usable retained-reference package, which may combine a protected physical reference, controlled files, test methods and first-batch records. A physical sample alone is not a measurable method. Bowlum's confirmed two-sided retained-sample process is specifically limited to housing-color customization, not claimed as a default for every order.
How should a buyer set batch-consistency tolerances?
Define them for the exact product, attribute, downstream use, test method and contract before the repeat-batch decision. This article does not publish generic color, brightness, pattern, dimensional or cosmetic tolerances because a number borrowed from another program can create false comparability.
Does roughly eight hours of factory aging prove batch consistency?
No. Bowlum confirms roughly eight hours of aging for every unit as a factory release control. It does not prove batch-to-batch equivalence, product life, field reliability, a defect rate or the absence of an unapproved change.
Does per-unit Class 1 release prove two projector batches are the same?
No. Bowlum's confirmed process requires applicable laser products to meet Class 1 before shipment. That unit-level release boundary does not prove optical sameness, transfer certification between models or replace the buyer's first/next-batch comparison.
What should happen when the repeat batch differs from the reference?
Preserve the exact identity, method, observation and evidence, then assign a disposition: accept as matched, correct and recheck, approve as a controlled change, or hold and escalate. If cause or defect pattern must be investigated, move that work into a separate evidence-based diagnosis record.